

Temperature Adaptation in Concrete Brick Production: Balancing Efficiency and Quality
The production efficiency of concrete brick machines is heavily dependent on environmental conditions; low and high-temperature operating environments present distinct technical challenges regarding equipment performance and brick molding. Adopting an environmental adaptation perspective, this paper systematically analyzes the core conflicts faced by concrete brick machines in these environments and proposes a balancing strategy anchored in three pillars: dynamic adjustment of process parameters, specialized equipment protection, and optimization of curing protocols. The central argument is that production efficiency and brick quality need not be a zero-sum game; precise environmental compensation strategies can ensure product strength and aesthetic quality while maintaining reasonable production output. In low-temperature environments, the balancing focus lies in heat management and ensuring proper hydration, whereas in high-temperature environments, the focus shifts to moisture control and the mitigation of thermal stress. The guiding principle for both scenarios is "proactive adjustment" rather than "reactive response."
I. Introduction
The production of concrete blocks and paving stones is essentially a coupled process involving cement hydration reactions and mechanical molding. This coupling is highly sensitive to ambient temperature and humidity; when temperatures deviate from the optimal range, changes occur in hydration rates, mixture workability, demolding quality, and even the stability of the equipment's hydraulic and lubrication systems.
In industry practice, a common tendency is to "trade quality for quantity" or "sacrifice quantity for quality"—either forcing full-load operation in harsh environments, leading to higher defect rates, or drastically slowing down production to the point of inefficiency. Neither strategy addresses the core issue: environmental adaptation is not about compromise, but rather about establishing differentiated process parameters and support systems tailored to specific temperature ranges.
The mechanisms by which low and high temperatures affect brick machine production differ fundamentally. The primary threats in low-temperature environments are water freezing and the stalling of chemical reactions, whereas in high-temperature environments, the main risks are rapid moisture evaporation and damage caused by thermal stress. Consequently, balancing strategies must be designed separately for each temperature range, with specific priorities for each. II. Balancing Strategies for Low-Temperature Environments
2.1 Key Impacts of Low Temperatures on Equipment and Bricks
When the ambient temperature drops below 5°C, concrete brick production faces multiple constraints. First, the viscosity of lubricating oil rises sharply as the temperature falls, increasing resistance in moving parts and making startup difficult; in severe cases, this causes sluggish hydraulic system response and unstable molding pressure. Second, the moisture within the mixture is at risk of freezing. Research indicates that when the temperature drops below 4.4°C, free water in the mortar begins to freeze, and the hydration reaction virtually stalls; the voids left by frozen water after thawing permanently weaken the brick's structural integrity.
Regarding brick quality, the most insidious risks of low-temperature production are "false set" and "frost damage"—where the green brick freezes before gaining sufficient strength, preventing it from ever reaching its design strength, even if curing conditions improve later. Canadian building codes explicitly mandate that when the air temperature is below 5°C, concrete must be maintained at a temperature of at least 10°C for 72 hours after placement.
2.2 Strategies for Adjusting Process Parameters
Preheating raw materials and optimizing the mix design are primary measures for low-temperature production. Mixing water should be heated (typically to 40–60°C) to compensate for heat loss absorbed by aggregates and cement. However, care must be taken to keep the water temperature below 60°C, as excessive heat can cause the cement to undergo "false set." Additionally, the use of early-strength agents or antifreeze admixtures can be considered to accelerate early strength development, allowing the bricks to reach critical strength before freezing occurs.
Dynamic adjustment of the molding cycle is equally critical. Low temperatures reduce the mixture's flowability; maintaining a standard molding cycle could result in uneven material distribution or inadequate compaction during vibration. Moderately extending the vibration time or adjusting the vibration frequency can compensate for the loss in workability without significantly sacrificing output. For specialized models in the industry with a standard molding cycle of approximately 25–30 seconds, the cycle can be extended by 2–3 seconds in low-temperature conditions rather than drastically reducing production volume.
2.3 Equipment Protection and Operational Strategies
The core strategy at the equipment level involves the coordination of lubrication systems and preheating procedures. In winter, hydraulic oil with good low-temperature fluidity and cold-resistant grease should be used to ensure the hydraulic system can rapidly build pressure during cold starts. The no-load preheating procedure prior to startup must not be skipped: the machine should idle for 3–5 minutes to allow the oil temperature to rise and lubrication to take effect before feeding materials.
Draining the hydraulic cooler to prevent freezing is a detail easily overlooked. If residual water remains in the cooler after operations cease, freezing overnight could cause the piping to burst. Anti-rust measures for molds and moving parts should also be intensified, as low-temperature condensation exacerbates the risk of corrosion on metal surfaces.
2.4 Curing Protocols
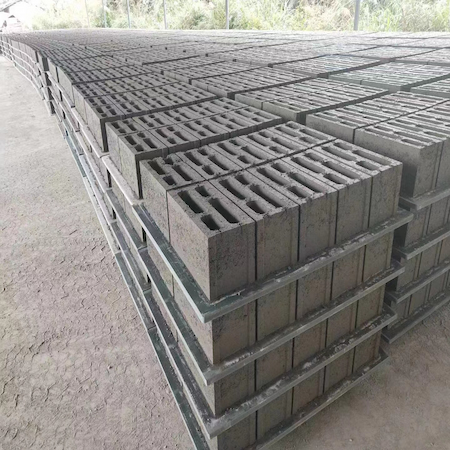
The key to low-temperature curing is prioritizing both thermal insulation and moisture retention. Finished bricks should not be cured naturally in the open air; instead, they should be placed in insulated sheds or covered with thermal insulation materials, utilizing the heat generated by cement hydration to maintain the curing temperature. Patented technologies demonstrate that a well-designed self-insulating curing system can maintain an internal curing temperature above 30°C even when the ambient temperature is 0°C, thereby significantly shortening the curing cycle.
Curing time must be substantially extended. While initial strength is achieved in 7 days at normal temperatures, it may take over 45 days to achieve the same result in low-temperature conditions. For factories with the necessary capabilities, steam curing or low-pressure steam environments can drastically reduce curing time; however, the rate of temperature rise must be controlled to prevent the bricks from cracking due to thermal stress.
III. Balancing Strategies for High-Temperature Environments
3.1 Key Impacts of High Temperatures on Equipment and Bricks
The primary technical challenge in high-temperature environments is the rapid loss of moisture. Stiff-consistency concrete has limited inherent water content; in environments exceeding 35°C, the mixture begins to lose significant moisture during mixing, conveying, and placement. Rapid surface evaporation leads to rough brick edges and insufficient strength development, potentially resulting in surface micro-cracks in severe cases.
Risks at the equipment level also cannot be ignored. When hydraulic oil temperatures exceed 60°C, viscosity drops and internal leakage increases, making it difficult to maintain stable control over molding pressure. Excessive temperatures inside electrical cabinets can trigger PLC malfunctions or accelerate component aging. Prolonged high-temperature operation also accelerates the degradation of seals and belts.
3.2 Process Parameter Adjustment Strategies
Moisture management is central to high-temperature production, yet "adding more water" is a dangerous misconception. While extra water may temporarily improve workability, it leads to issues such as bricks sticking to molds, deformation, and inconsistent heights. The correct strategy is to compensate for evaporation rather than altering the water-cement ratio: shorten the time interval between mixing and molding, provide shading for conveyors, and—when necessary—use misting rather than direct water injection to maintain ambient humidity.
Aggregate management is equally critical. Under high-temperature conditions, the surface temperature of sand and gravel can exceed 50°C; without shading at the aggregate storage yard, the temperature of the mixture entering the mold will be excessively high. Pre-wetting aggregates or storing them under shade can effectively lower the initial temperature of the mixture.
3.3 Equipment Heat Dissipation and Operational Strategies
Thermal management of hydraulic systems requires systematic monitoring. Industry-recommended standards dictate that a warning should be issued when hydraulic oil temperatures exceed 60°C, and motor operating temperatures should be kept below 75°C. For brick machines in continuous operation, hydraulic stations must be equipped with effective cooling systems, and radiators should be inspected regularly for dust-related blockages.
Protection of electrical cabinets is crucial. The combination of high temperatures and dust accelerates electrical failures; therefore, ensure cooling fans operate correctly, keep ventilation vents unobstructed, and regularly remove accumulated dust. In regions with extreme heat, installing industrial air conditioning units for active cooling of electrical cabinets should be considered.
3.4 Curing Protocols
The key to curing in high-temperature conditions is preventing premature dehydration. If freshly demolded brick units are exposed directly to sunlight and hot, dry winds, surface moisture can evaporate completely within hours, halting cement hydration due to water deficiency. Research indicates that initial curing of concrete blocks in high-temperature environments should avoid direct sunlight, with the first 24 hours being particularly critical. Effective strategies include establishing shaded curing zones, using moisture-retaining coverings, and installing misting systems in curing areas to maintain humidity. It is important to note that in high-temperature conditions, the curing water itself is often hot; direct spraying could exacerbate temperature fluctuations within the bricks. A safer approach is to allow the green bricks to rest in a cool, shaded area after demolding—letting surface moisture evaporate moderately and the bricks develop initial structural integrity—before commencing moisture-retention curing.
IV. Principles of Comprehensive Balance and Industry Practice
4.1 Proactive Adjustment vs. Reactive Response
Whether dealing with low or high temperatures, the core philosophy of environmental adaptation is "proactive intervention." For low-temperature production, tasks such as changing lubricants, deploying thermal insulation, and conducting staff training should be completed before winter sets in. Conversely, high-temperature production requires checking hydraulic heat dissipation, electrical cooling systems, and shading conditions in curing areas before summer arrives. When environmental parameters exceed controllable limits, proactively reducing production capacity—rather than risking full-load operation—is the more economical choice.
4.2 Environmental Adaptability in Equipment Selection
From a long-term operational perspective, a machine's ability to adapt to the environment should be a key criterion during selection. For extreme cold, using low-temperature-resistant steel for the vibration table ensures stable output at -40°C; for high-temperature environments, critical parameters to evaluate include the heat dissipation redundancy of the hydraulic system and the electrical protection rating. Global industry experience demonstrates that equipment designed for environmental adaptability maintains stable operation even under harsh conditions.
4.3 The True Relationship Between Quality and Output
The ultimate goal of environmental adaptation is to maximize output while adhering to quality constraints under specific environmental conditions—avoiding both a blind obsession with volume and an unrealistic pursuit of perfection. Reducing output by 20% in cold weather to prevent frost damage is far more economical than running at full capacity while seeing the defect rate rise by 40%. Similarly, sacrificing a small amount of cycle time in high temperatures to ensure demolding integrity and dimensional stability is a rational choice.
V. Conclusion
Operating concrete brick machines in low- or high-temperature environments is, fundamentally, a process of working in harmony with the laws of physics. In low-temperature conditions, the core challenges are hydration stagnation and the risk of freezing caused by insufficient heat; in high-temperature conditions, the primary issues are moisture loss and the accumulation of thermal stress. While specific mitigation strategies differ for each scenario, they share a common logic: achieving a dynamic optimum between environmental constraints and production goals through the dynamic adjustment of process parameters, specialized equipment protection, and strengthened curing protocols.
Adapting to environmental conditions is not merely a passive constraint on production efficiency but a proactive investment in the robustness of the production system. For brick manufacturing plants operating year-round, the implementation of standardized operating procedures tailored to specific seasons and temperature zones yields returns in the form of reduced defect rates, extended equipment lifespan, and more reliable order fulfillment.
To get a custom solution or request a quote, please visit https://www.yxbrickequipment.com